INDUSTRIAL PRODUCT
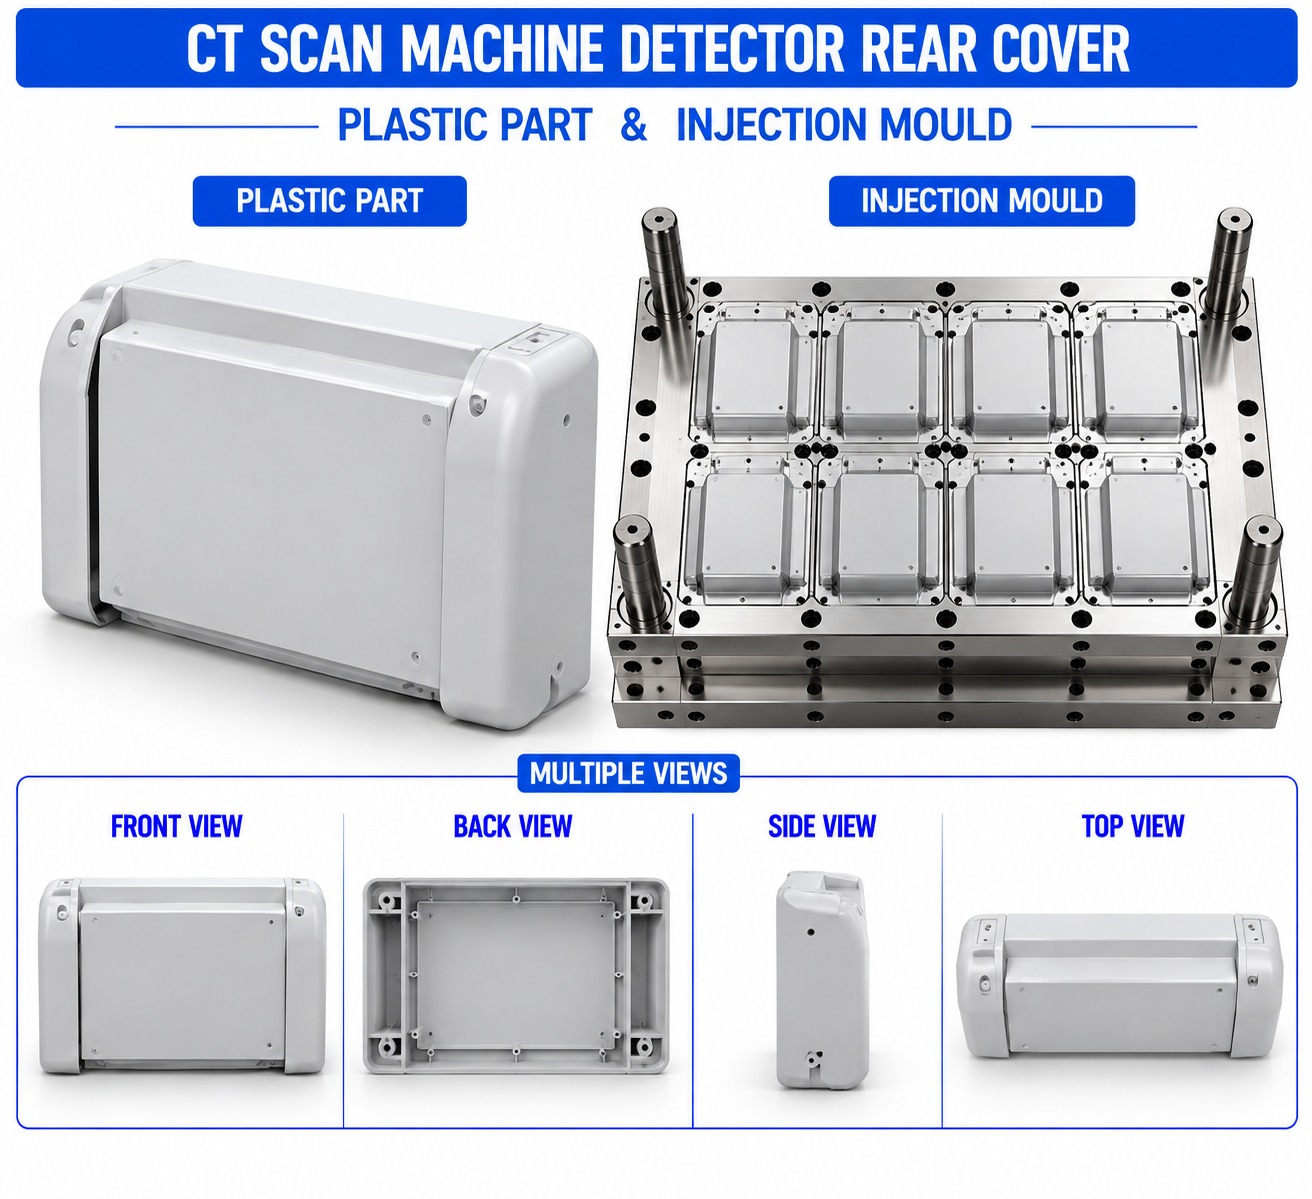
CT Scan Machine Plastic Detector Rear Cover Mould and Moulding Service
₹800.00
CT Scan Machine Plastic Detector Rear Cover Mould and Moulding Service | Renovator Appliances Ltd
Product Overview
Renovator Appliances Ltd manufactures precision Plastic Injection Moulds and provides injection moulding solutions for CT Scan Machine Plastic Detector Rear Cover components used as protective and finishing enclosure sections on the rear side of designated CT detector assemblies. The rear cover helps protect internal detector-related components while providing a finished enclosure surface and maintaining the required interfaces for adjoining covers, mounting structures, cables, connectors, ventilation, and surrounding gantry components.
The mould is developed according to the detector assembly dimensions, rear profile, curvature, mounting arrangement, internal component clearance, cable-routing requirements, ventilation provisions, service-access requirements, and adjoining housing geometry. The CT Scan Machine Plastic Detector Rear Cover can be customized with mounting bosses, locating ribs, retaining clips, snap-fits, cable openings, connector clearances, ventilation openings, and other product-specific features.
Key Features
Precision injection moulding for consistent detector rear-cover production
Customized rear-cover profile according to detector assembly geometry
Accurate fitment with detector front, side, and adjoining covers
Controlled internal clearance for detector components
Integrated mounting bosses and locating features
Screw-fit, clip-fit, or snap-fit assembly options
Cable and connector clearance provisions
Optional ventilation openings and grille sections
Reinforcing ribs for improved housing rigidity
Controlled wall thickness for dimensional stability
Smooth and consistent exterior surface
Customized colour, texture, and surface finish
Suitable for prototype development and volume production
Supports OEM and ODM manufacturing requirements
Industrial Applications
| Application | Use of CT Scan Machine Plastic Detector Rear Cover |
|---|---|
| CT Detector Assembly | Provides rear enclosure protection for designated detector components |
| CT Gantry Detector System | Integrates with the rear section of the detector housing |
| Detector Electronics Enclosure | Protects designated internal components, wiring, and connectors |
| Medical Imaging Equipment | Provides a finished protective enclosure surface |
| CT Service Assembly | Supports service access and enclosure integration where required |
| OEM CT Scanner Equipment | Manufactured according to customized detector housing designs |
Manufacturing Process
1. Product Design & Development
The CT Scan Machine Plastic Detector Rear Cover is developed according to the customer's CAD drawing, 3D model, physical sample, detector assembly, or equipment specifications. The design is reviewed for overall dimensions, rear profile, curvature, wall thickness, adjoining-cover interfaces, mounting locations, internal component clearance, cable routing, connector access, ventilation, and service requirements.
2. Plastic Mould Design
The injection mould is designed according to the rear-cover geometry and required assembly features. The mould incorporates suitable parting lines, draft angles, gate locations, cooling channels, ejector arrangements, cores, inserts, and shrinkage allowances.
For large or curved rear covers, balanced filling and cooling are considered to minimize warpage, distortion, sink marks, and dimensional variation. Mounting bosses, locating ribs, snap-fit features, ventilation openings, cable passages, and connector clearances are positioned according to the complete detector assembly.
3. Mould Manufacturing
Mould components are manufactured using suitable mould steels such as P20 Steel, H13 Steel, or S136 Steel according to production quantity, expected mould life, selected plastic material, surface-finish requirements, and component complexity. CNC machining, EDM, drilling, grinding, polishing, fitting, and mould assembly are used to achieve accurate cavity geometry.
4. Injection Moulding
The selected plastic material is processed using controlled injection moulding parameters. Injection temperature, filling speed, injection pressure, holding pressure, cooling time, and cycle time are adjusted according to the selected plastic grade and rear-cover design.
Controlled processing helps maintain rear-cover profile accuracy, mounting-feature alignment, ventilation-opening dimensions, wall-thickness consistency, surface quality, and dimensional stability.
5. Finishing & Assembly Preparation
After moulding, the detector rear covers are inspected for flash, gate marks, sink marks, short shots, sharp edges, and surface imperfections. Mounting bosses, screw holes, locating features, cable openings, connector clearances, ventilation sections, and adjoining-cover interfaces are checked before assembly.
Where required, the moulded cover can be prepared for labels, identification markings, surface decoration, or installation with the corresponding detector housing components.
6. Quality Inspection
Finished CT Scan Machine Plastic Detector Rear Cover components are checked for overall dimensions, rear profile, curvature, mounting alignment, adjoining-cover fitment, internal clearance, ventilation openings, surface finish, and assembly accuracy.
Trial assembly with the designated detector housing can be performed to verify proper alignment, fastening, cable clearance, connector access, ventilation clearance, and interference-free integration with surrounding CT scanner components.
Raw Materials
| Material | Suitability for CT Scan Machine Plastic Detector Rear Cover |
|---|---|
| ABS | Suitable for rigid detector enclosure covers requiring good surface appearance |
| PC+ABS | Suitable where improved impact resistance and dimensional stability are required |
| PC | Suitable where higher impact and temperature performance are required |
| PP | Lightweight option with good moisture and chemical resistance |
| HIPS | Suitable for economical rigid enclosure applications where specifications permit |
| PBT | Suitable where good dimensional stability and temperature performance are required |
| Flame-Retardant ABS | Suitable where specified flame-performance requirements apply |
| Flame-Retardant PC+ABS | Suitable for applications requiring enhanced fire performance |
| Engineering-Grade Plastic | Suitable for demanding mechanical, thermal, dimensional, or environmental requirements |
The final plastic grade should be selected according to mechanical requirements, operating temperature, cleaning and disinfectant exposure, dimensional stability, surface requirements, electrical environment, flame-performance requirements, and applicable medical-device specifications.
Quality Control
Renovator Appliances Ltd performs quality checks throughout mould development and injection moulding production. Inspection can include:
Plastic material and grade verification
Mould cavity dimensional inspection
Overall rear-cover dimensions
Rear profile and curvature inspection
Wall-thickness consistency
Mounting-boss position
Screw-hole dimensions where applicable
Locating-rib accuracy
Clip and snap-fit accuracy
Cable-opening dimensions
Connector clearance
Ventilation-opening dimensions
Internal component clearance
Adjoining-cover alignment
Warpage and deformation inspection
Sink-mark and short-shot inspection
Flash and burr inspection
Surface-finish inspection
Colour consistency
Label or marking-area inspection where applicable
Detector housing trial assembly
Fitment and alignment verification
Ventilation-path clearance where applicable
Batch-to-batch dimensional consistency
Buyer Guide
When ordering CT Scan Machine Plastic Detector Rear Cover Mould and Moulding Service, buyers should provide the detector housing design or relevant component specifications. Important requirements include:
Detector assembly dimensions
Rear-cover profile and curvature
Front, side, and adjoining-cover interface dimensions
Required wall thickness
Mounting-hole locations
Screw, clip, or snap-fit requirements
Internal detector-component clearance
Cable and connector locations
Ventilation-opening requirements
Required service-access provisions
Adjacent gantry-component clearance
Plastic material and grade
Flame-performance requirements where applicable
Colour and surface texture
Surface-finish requirements
Expected production quantity
Required mould life
Prototype or mass-production requirements
OEM or ODM assembly requirements
For CT scanner equipment, the Detector Rear Cover should be validated as part of the complete medical-device assembly for mechanical fitment, thermal conditions, cleaning and disinfectant exposure, EMC considerations, detector-related clearances, imaging-related requirements, radiation safety, and applicable regulatory requirements. The plastic detector rear cover should not be assumed to provide radiation shielding or define the X-ray beam unless specifically engineered, tested, and validated for that purpose.
Why Choose Renovator Appliances Ltd?
Advanced Injection Moulding Facility
Renovator Appliances Ltd provides controlled plastic injection moulding for precision medical-equipment enclosure components requiring accurate profiles, mounting features, ventilation provisions, internal clearances, and consistent surface quality.
In-House Mould Manufacturing
In-house mould manufacturing provides better control over rear-cover geometry, adjoining interfaces, mounting features, cooling, ejection, ventilation openings, surface finish, and dimensional accuracy.
OEM & ODM Manufacturing
Customized CT Scan Machine Plastic Detector Rear Cover moulds and moulded components can be developed according to customer drawings, detector samples, housing designs, and complete equipment specifications.
Quality Assurance
Dimensional, visual, material, assembly, and fitment checks help maintain consistent detector rear-cover quality and integration with the complete CT scanner assembly.
Cost-Effective Manufacturing
Integrated mould manufacturing and injection moulding support efficient production for prototype development as well as regular commercial quantities.
Frequently Asked Questions
1. What is a CT Scan Machine Plastic Detector Rear Cover?
It is a moulded plastic enclosure component designed to provide rear protection and finished housing coverage around a designated CT detector assembly.
2. Can the detector rear cover be customized according to the detector housing?
Yes. The rear profile, curvature, dimensions, mounting features, cable openings, connector clearances, ventilation provisions, and adjoining-cover interfaces can be customized according to the detector assembly.
3. Can ventilation openings and mounting features be incorporated?
Yes. Ventilation openings, screw bosses, mounting holes, locating ribs, clips, snap-fits, cable passages, and other assembly features can be integrated into the mould according to the equipment design.
4. Which plastic materials can be used for the detector rear cover?
ABS, PC+ABS, PC, PP, HIPS, PBT, flame-retardant ABS, flame-retardant PC+ABS, and suitable engineering plastics can be considered according to mechanical, thermal, dimensional, cleaning, and equipment requirements.
5. Can Renovator Appliances Ltd manufacture both the mould and moulded detector rear cover?
Yes. Renovator Appliances Ltd can provide mould design, mould manufacturing, injection moulding, prototype development, quality inspection, and volume production support for customized CT Scan Machine Plastic Detector Rear Cover components.
- SKU
- REN-EFCDE7435F7E2732AE3A72A0